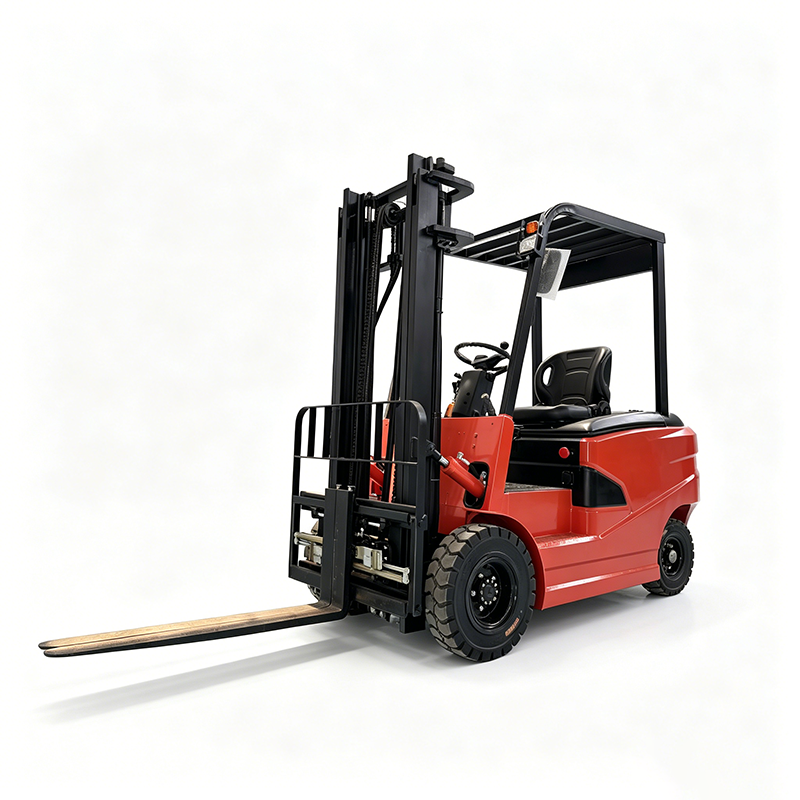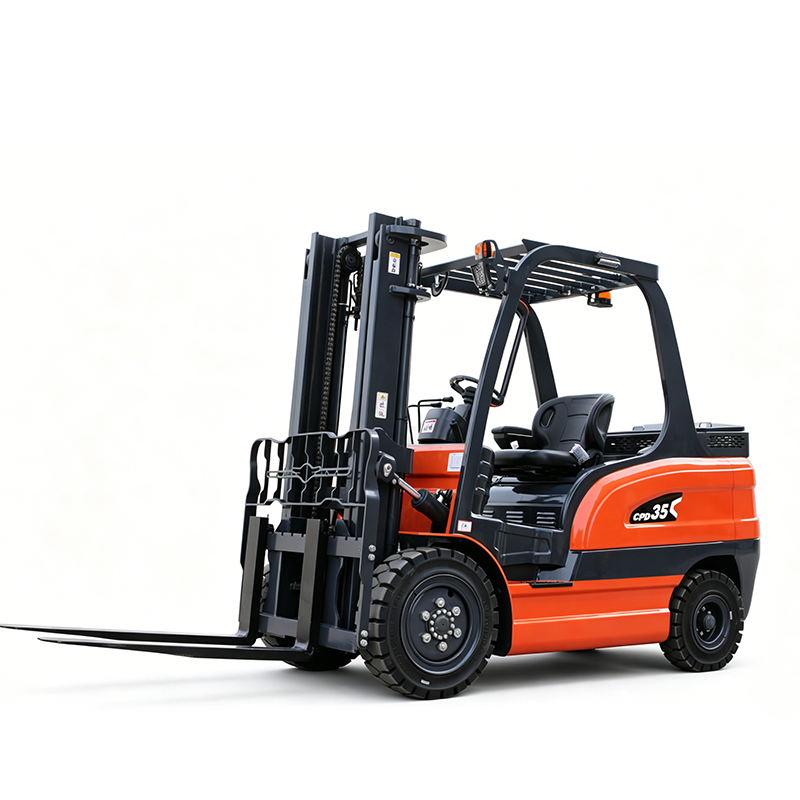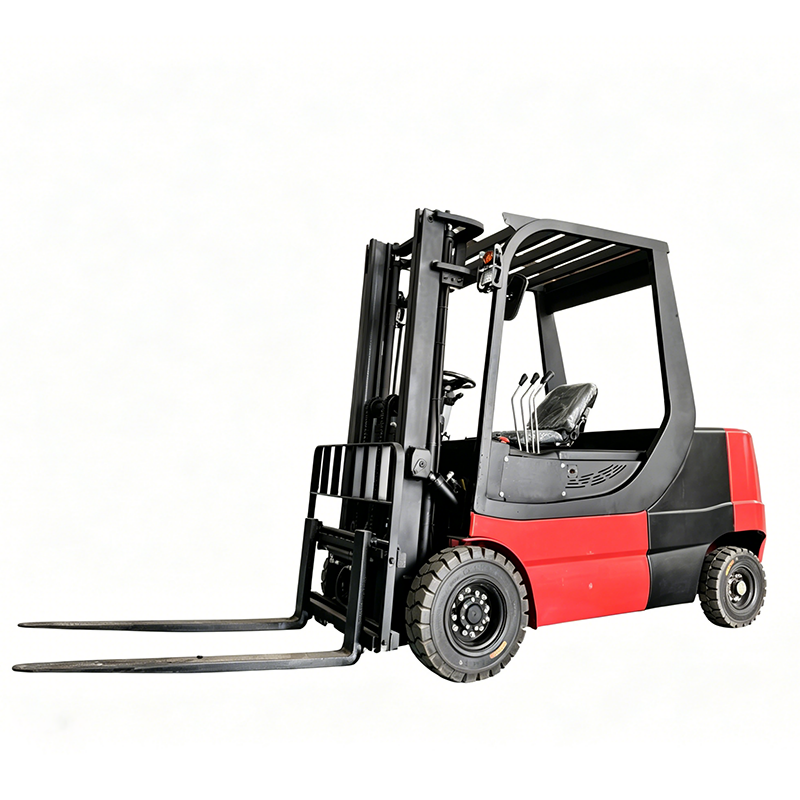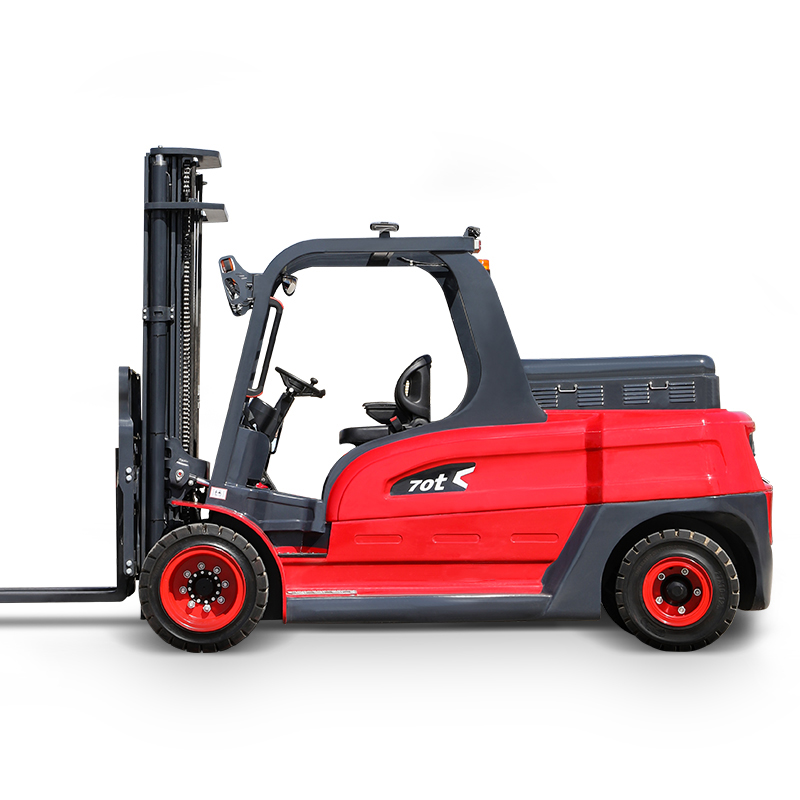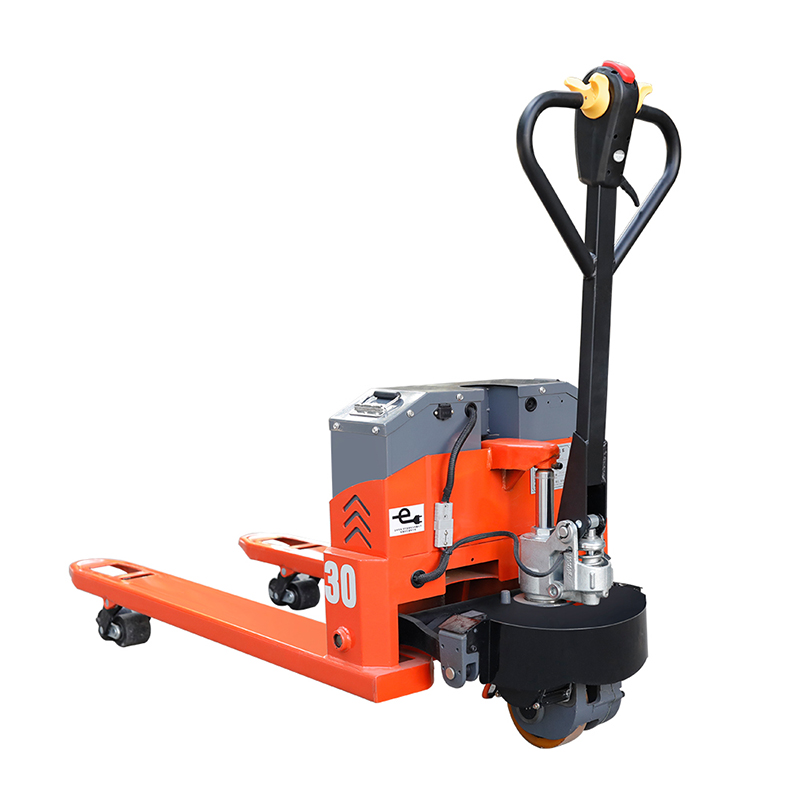
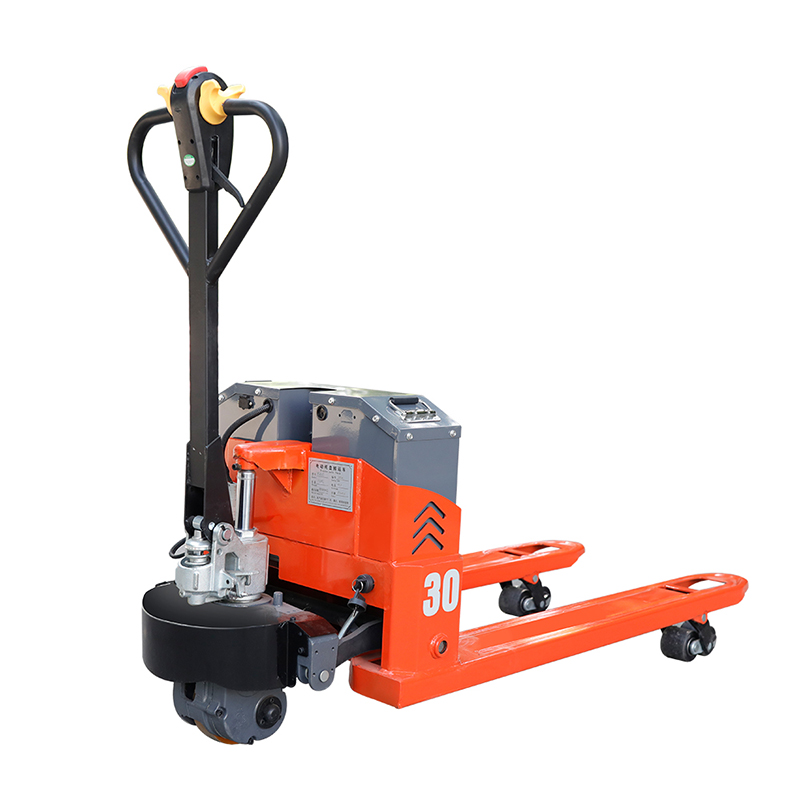
Electric forklift pallet trucks have revolutionized material handling by offering a cleaner, more efficient alternative to traditional internal combustion models. These vehicles are powered by electric batteries, which significantly reduce greenhouse gas emissions and eliminate harmful fumes, making them ideal for indoor applications like warehouses, factories, and retail distribution centers. With the increasing global emphasis on environmental sustainability, businesses are transitioning to electric fleets not only to meet regulatory requirements but also to reduce long-term operational costs. The operational benefits extend beyond environmental impact; electric pallet trucks provide instant torque delivery, which enhances acceleration and lifting speed, thereby improving cycle times and overall throughput. Moreover, advancements in battery technology, particularly the adoption of lithium-ion cells, have addressed the historical limitations of electric trucks, such as long charging times and limited range. Lithium-ion batteries now offer high energy density, enabling longer shifts, and they feature opportunity charging capabilities that allow for quick top-ups during breaks. Additionally, the total cost of ownership for electric pallet trucks is lower than for internal combustion units, as they have fewer moving parts, do not require regular oil changes, and benefit from reduced fuel and maintenance expenses. The ergonomic design of modern electric pallet trucks also prioritizes operator comfort and safety, contributing to lower fatigue and fewer workplace accidents. In a global market where efficiency and sustainability are paramount, investing in an electric forklift pallet truck represents a strategic move that aligns with future operational trends. Shandong Kaiyite Machinery’s electric pallet trucks are engineered to meet diverse industrial needs, offering customizable options such as different load capacities, platform types, and battery configurations, ensuring optimal performance for specific applications. With global certifications and robust after-sales support, they stand as a testament to quality and innovation, empowering businesses to achieve their material handling goals more effectively.
06
Jul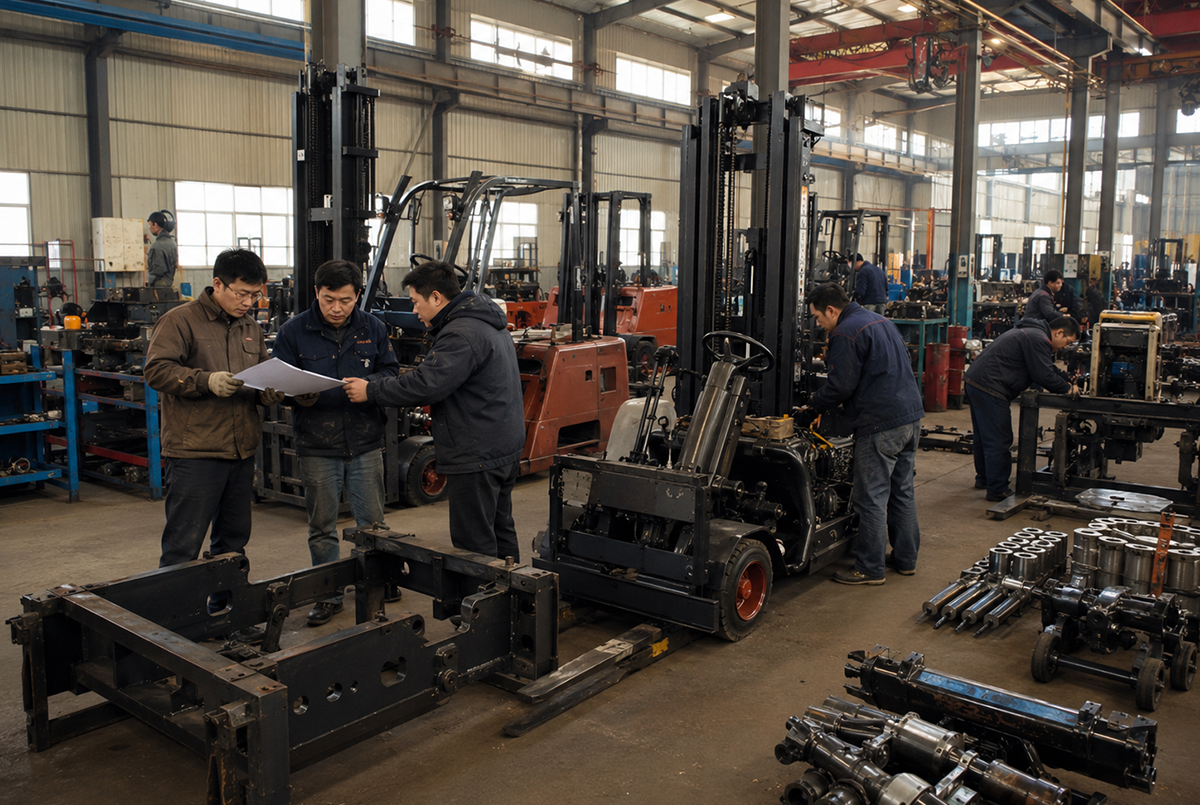
09
Jul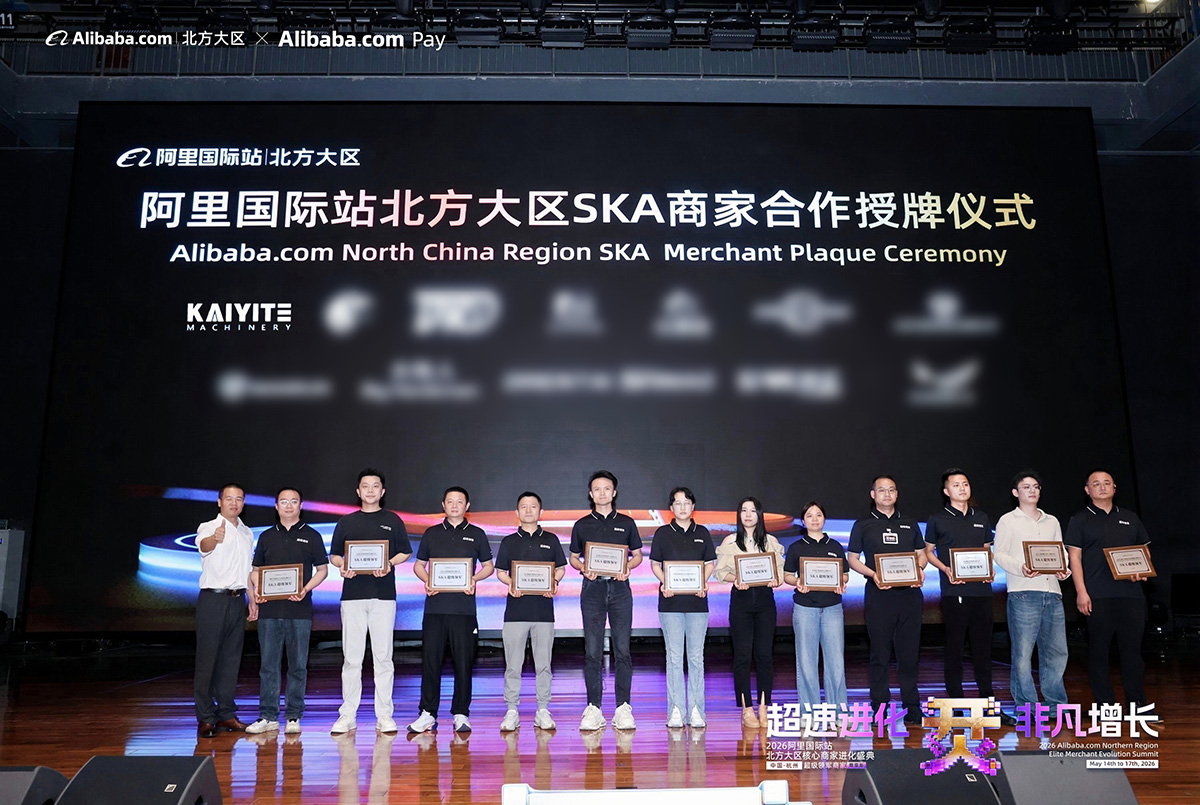
29
Jul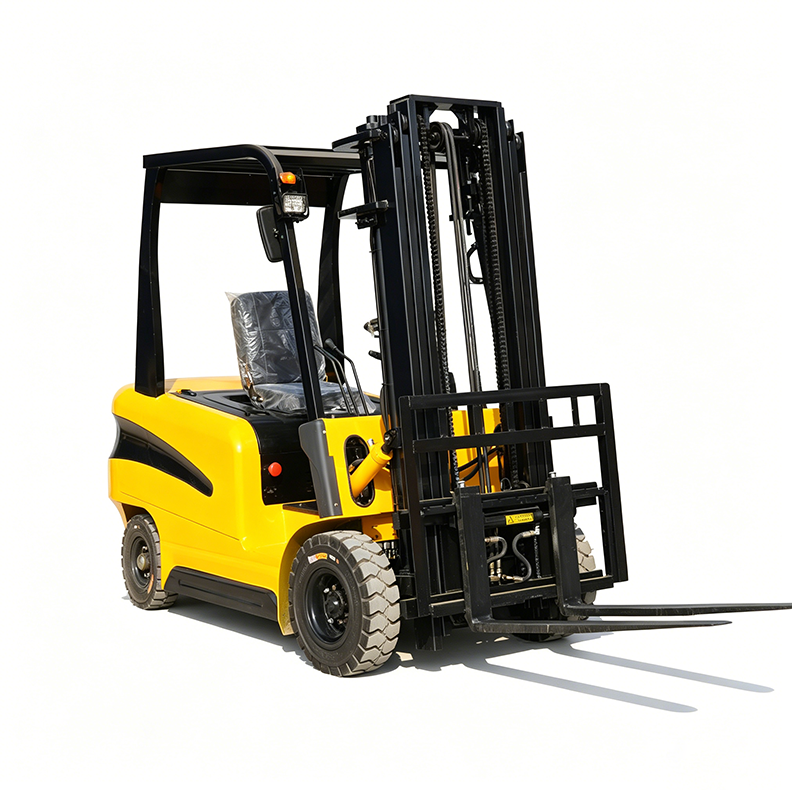
17
Sep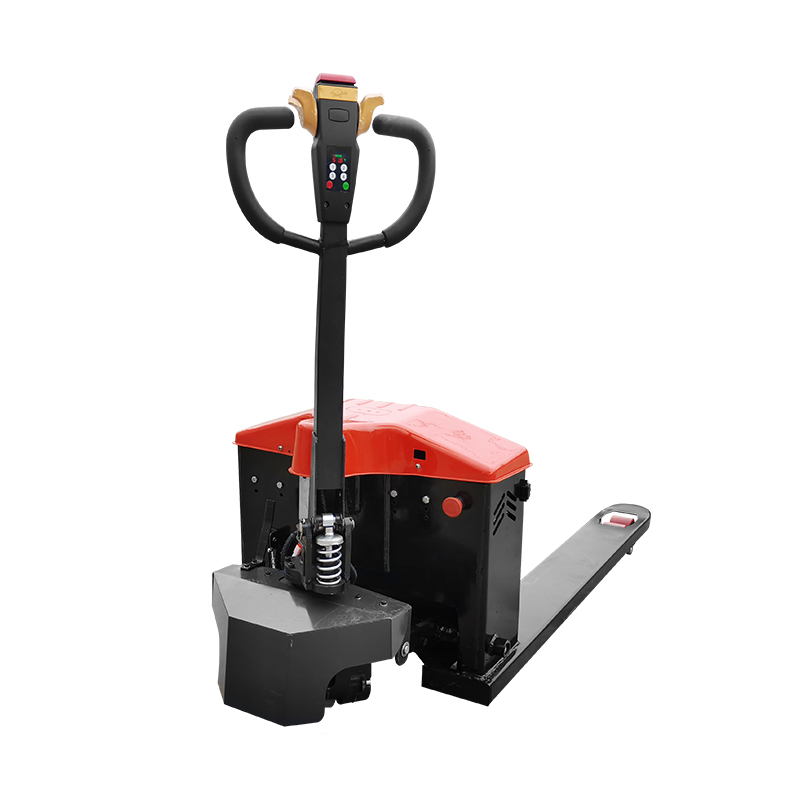
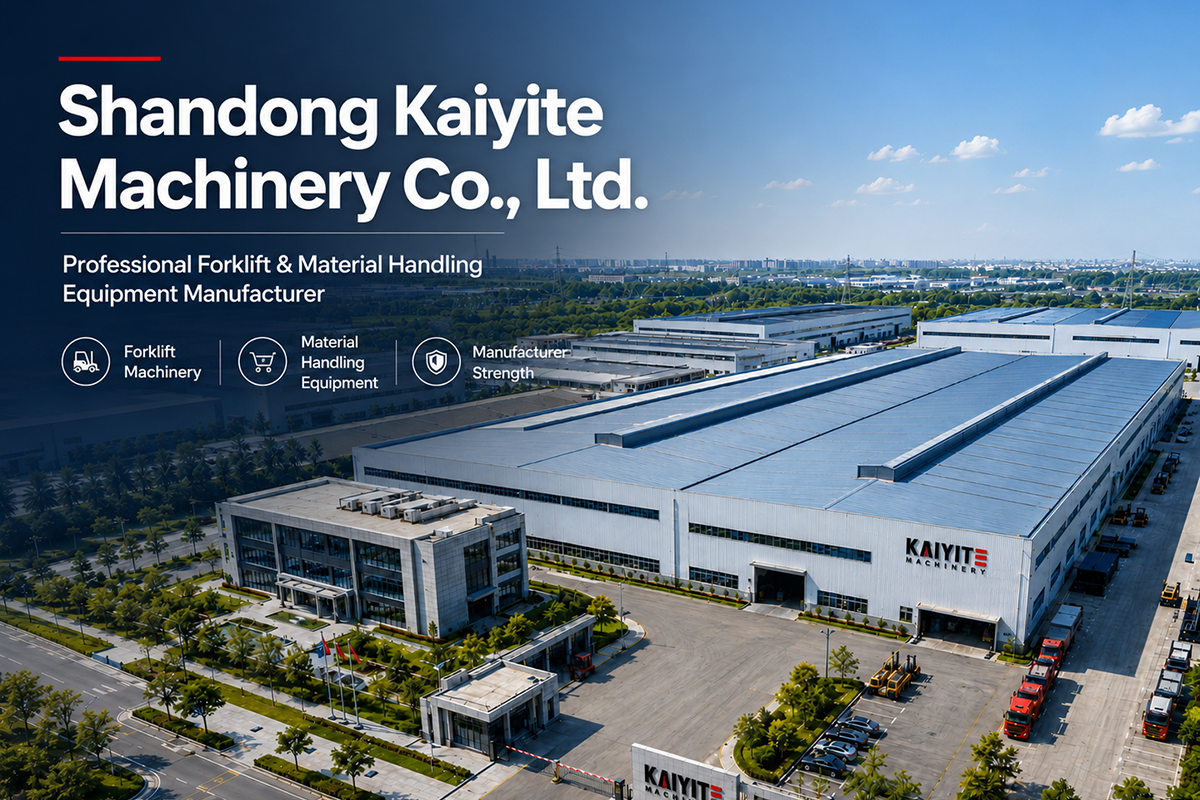
Shandong Kaiyite Machinery is an important participant in the construction machinery industry, located in a city known for well-known forklift brands such as Komatsu and Toyota. The factory covers an area of 128000 square meters and currently has over 1800employees, including 390 engineers.
Room 1314, 13th Floor, Block B, Zhongde Plaza, Liying Street, Rencheng District, Jining City, Shandong Province
 Wechat QRCode
 WhatsApp
Copyright © 2026 by Shandong Kaiyite Machinery Co., Ltd. Privacy Policy
 EN